Contact surfaces and fastening conditions
Electrical connections are designed around surface preparation, mating materials and tightening torque.

Innozinc is a surface-treatment technology that addresses corrosion resistance, tensile-load performance and dimensional precision in power hardware, including pole-anchor U-bolts and crossarm shackles. Production performance assessment with a Korean power-equipment manufacturer met all 12 evaluation targets. Thin plating and an ambient-temperature process improve fastening quality and manufacturing efficiency.
Power hardware must combine corrosion protection, mechanical integrity and reliable electrical connections within the specified product dimensions.
Inspection and replacement of ground-line and overhead structures must account for operating equipment and planned outages. Managing corrosion exposure and connection quality at the surface-treatment stage improves maintenance efficiency.
Localized corrosion control at ground-line and buried sectionsProduction performance assessment of pole-anchor U-bolts and crossarm shackles confirmed performance equivalent to or better than the existing hot-dip galvanized products. Corrosion and post-exposure tensile-performance data support the adoption of Innozinc specifications for power hardware.
Assessment conditions and results belowFor grounding and bonding hardware, electrical continuity and contact resistance are critical quality characteristics. Assessment conditions reflect the contact surfaces, mating materials and tightening torque of the actual Innozinc-plated assembly, including connection quality before and after environmental exposure.
Assembly contact resistance and electrical continuityPlating specifications are developed around the required coating process, thickness and corrosion performance. KEMP supports customer approval with product-specific performance data and sample assessment.
Product-specific specifications and assessment supportInnozinc-plated pole-anchor U-bolts and crossarm shackles were assessed for corrosion resistance, tensile-load performance and fabrication properties. The 2025 materials, components and equipment production performance assessment met all 12 targets. The evaluated products demonstrated performance equivalent to or better than their hot-dip galvanized counterparts.
| Specimen / Product | Test Characteristic | Target / Condition | Result |
|---|---|---|---|
| Plated specimen | Erichsen cupping | ≥10 mm | 12.2 mm |
| Plated specimen | Impact resistance | No surface defects | No defects |
| Plated specimen | Abrasion resistance / mass loss | ≤25 mg | 21 mg |
| Plated specimen | Coating thickness | ≥8 μm | 13 μm |
| Crossarm shackle | Neutral salt spray | 600 hr | No red rust |
| Crossarm shackle | Cyclic corrosion | 40 cycle | No red rust |
| Crossarm shackle | Tensile load | 39.20 kN | No surface defects |
| Crossarm shackle | Stress cracking after corrosive exposure | Compared with the existing hot-dip galvanized product | Equivalent or better |
| Pole-anchor U-bolt | Neutral salt spray | 600 hr | No red rust |
| Pole-anchor U-bolts | Cyclic corrosion | 40 cycle | No red rust |
| Pole-anchor U-bolts | Tensile load | 39.20 kN | No surface defects |
| Pole-anchor U-bolts | Stress cracking after corrosive exposure | Compared with the existing hot-dip galvanized product | Equivalent or better |
Source: 2025 Production Performance Assessment Confirmation for Materials, Components and Equipment (31 Dec 2025). Results apply to the plated specimens, crossarm shackles and pole-anchor U-bolts evaluated in that project.
Innozinc's thin, uniform deposit and ambient-temperature plating process improve dimensional control of threaded joints and downstream fabrication efficiency. They deliver surface-treatment quality for power hardware such as pole-anchor U-bolts and crossarm shackles.
| Design / Manufacturing Requirement | Innozinc Advantage | Application Detail |
|---|---|---|
| Mechanical performance after corrosive exposure | Production performance targets met | Tensile-load and stress-cracking assessment of pole-anchor U-bolts and crossarm shackles |
| Plating thickness control | 13 μm measured on the assessed specimen | Target ≥8 μm · Target thickness specified by product |
| Threaded joints | Dimensional control through thin plating | Plating conditions set against thread tolerances and gauge requirements |
| Process temperature | Ambient-temperature plating reduces thermal distortion | Electrodeposition at approximately 25 °C · Post-treatment defined by the application specification |
| Protection of fabricated surfaces | Complete surface treatment after fabrication | Plating after cutting and punching treats exposed fabricated surfaces |
| Environmental requirements | Hexavalent-chromium-free specifications | Post-treatment aligned with product-specific environmental requirements |
The measured 13 μm deposit and ambient-temperature plating process support dimensional control of threaded joints and reduced thermal distortion. KEMP specifies plating, pretreatment and post-treatment for each material, strength grade and thread tolerance.
Innozinc combines an electrodeposited zinc layer with an inorganic composite film. Grounding and bonding specifications are established by assessing contact resistance and corrosion performance in the actual assembly.
Electrical connections are designed around surface preparation, mating materials and tightening torque.
Initial contact resistance and changes after corrosion or environmental exposure are assessed against customer acceptance criteria.
Pretreatment, plating and post-treatment are specified by material and strength grade. For high-strength components, hydrogen-embrittlement controls and process qualification are established before production.
Rack plating (35 t/day) handles long and large components; barrel plating (7 t/day) processes hardware and fasteners.

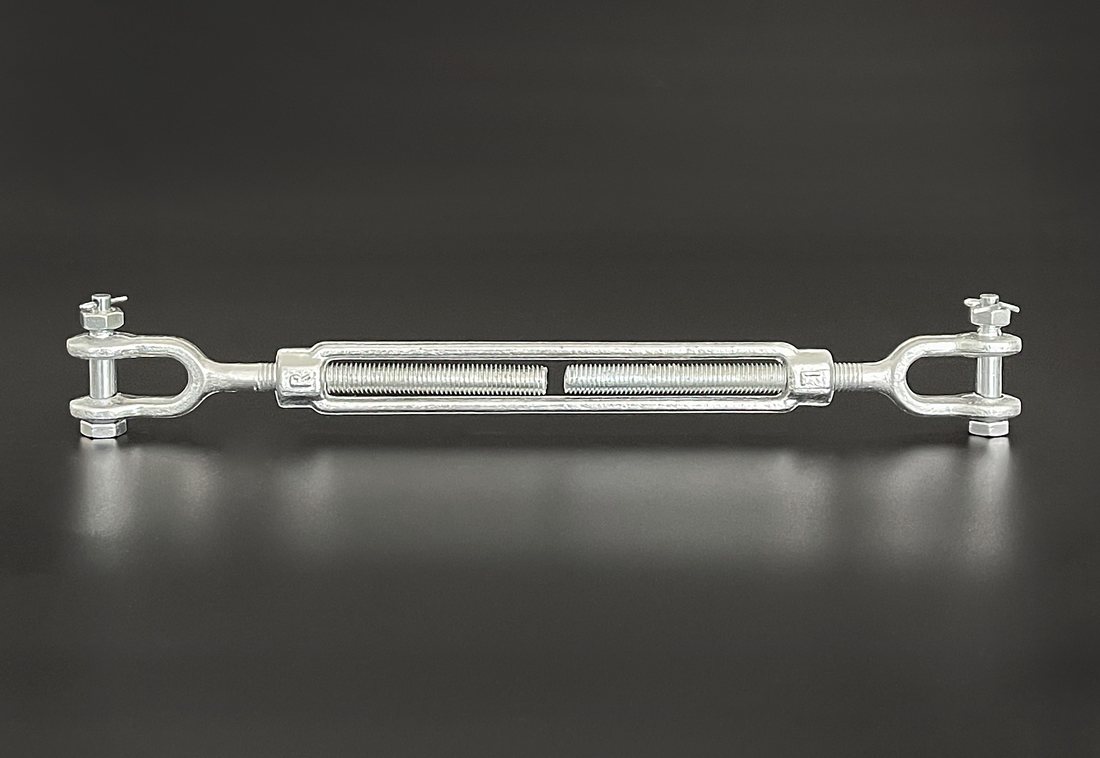
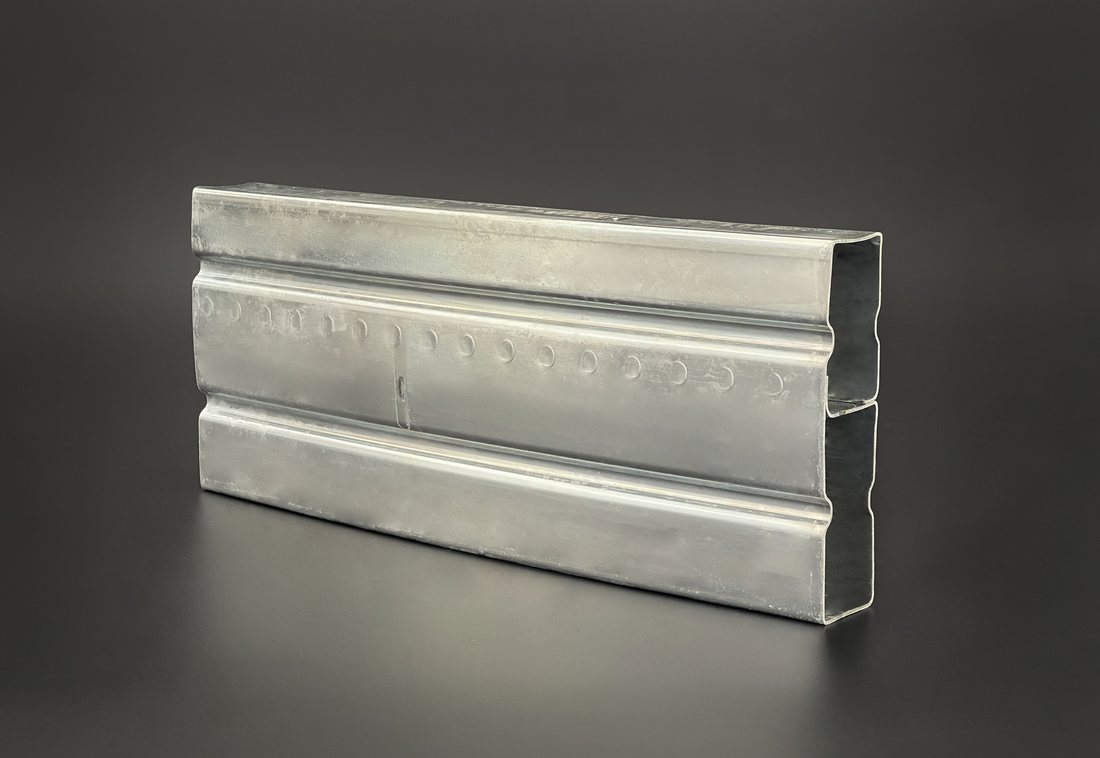

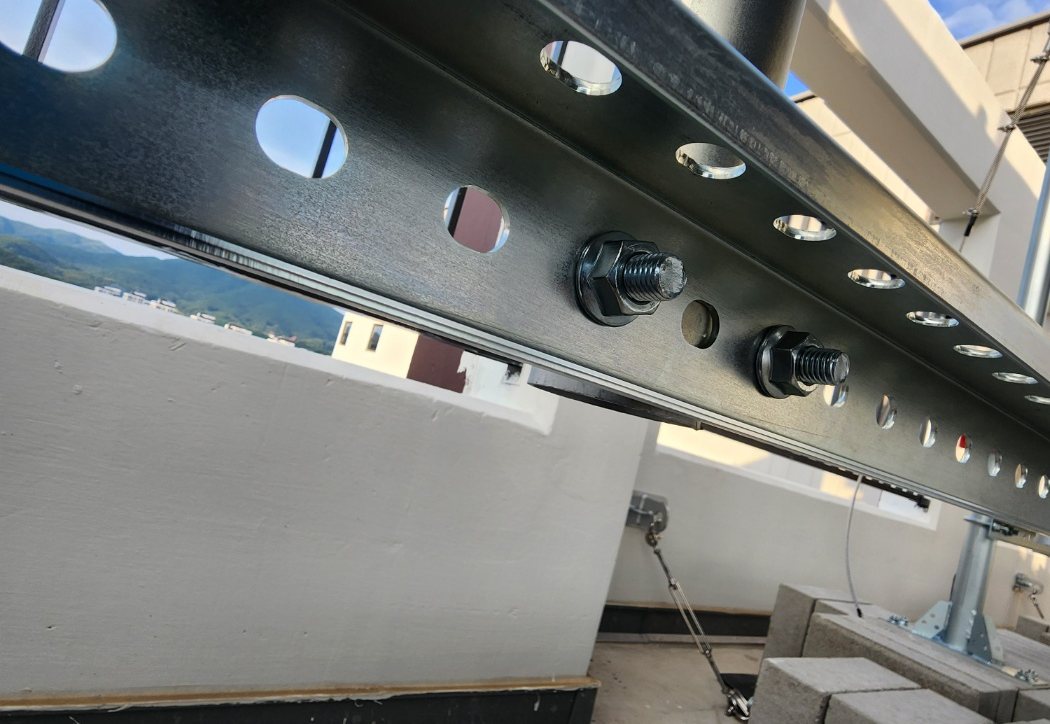
| Product | Exposure Conditions | Recommended Specification | Application / Assessment Criteria |
|---|---|---|---|
| Pole-anchor U-bolts · Nuts · Washers | Buried and ground-line exposure | Innozinc | Product assessed in the production performance program, including bent sections |
| Crossarm shackles · Ball shackles | Outdoor overhead exposure | Innozinc | Tensile-load testing completed |
| Crossarm bands · Arm ties · Line hardware | Outdoor overhead exposure | Innozinc | Complex geometries with controlled coating-thickness variation |
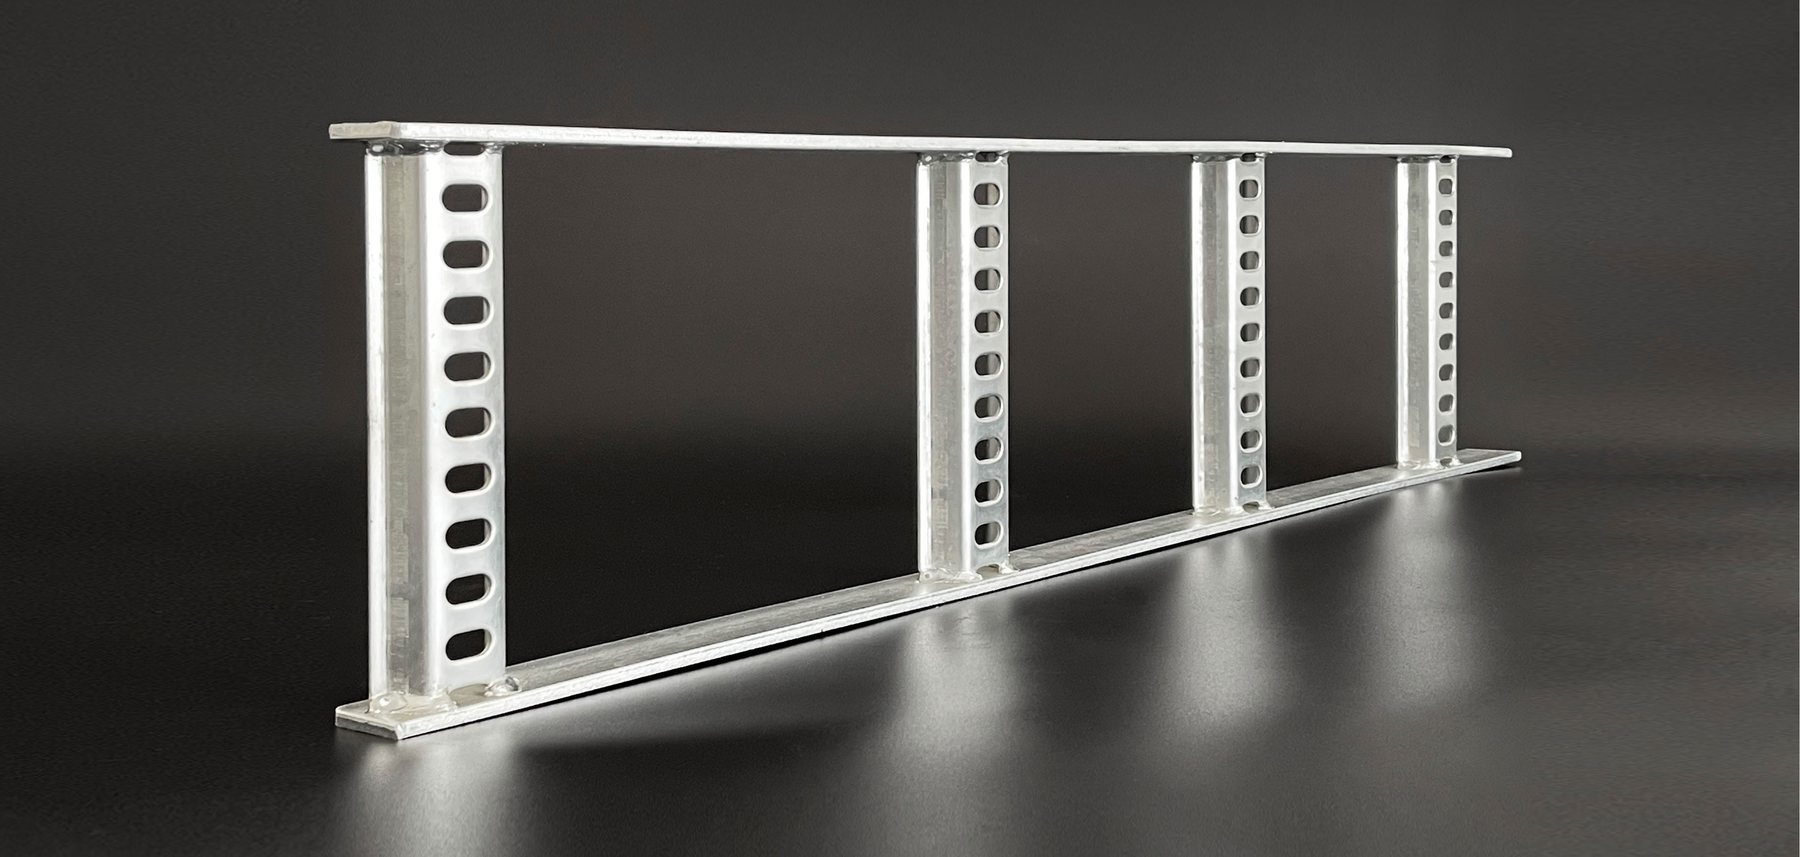
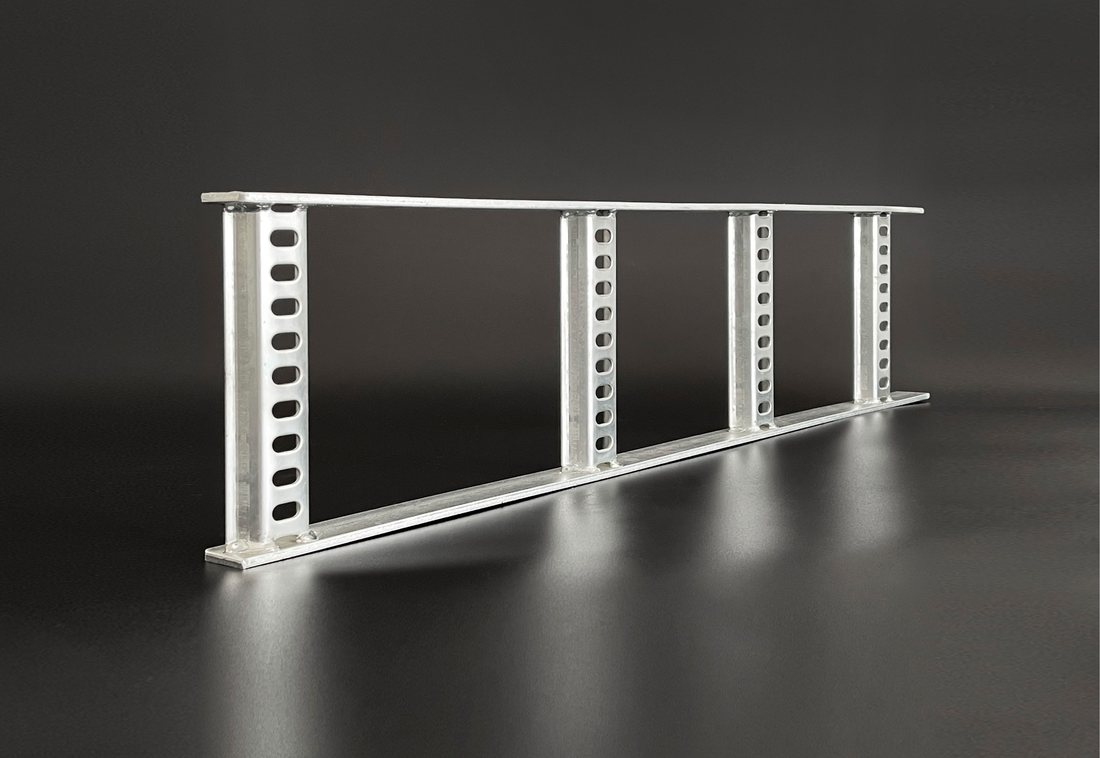
| Cable trays · Ladders · Ducts | Indoor / Outdoor | Innozinc | Plating integrated after cutting and punching |
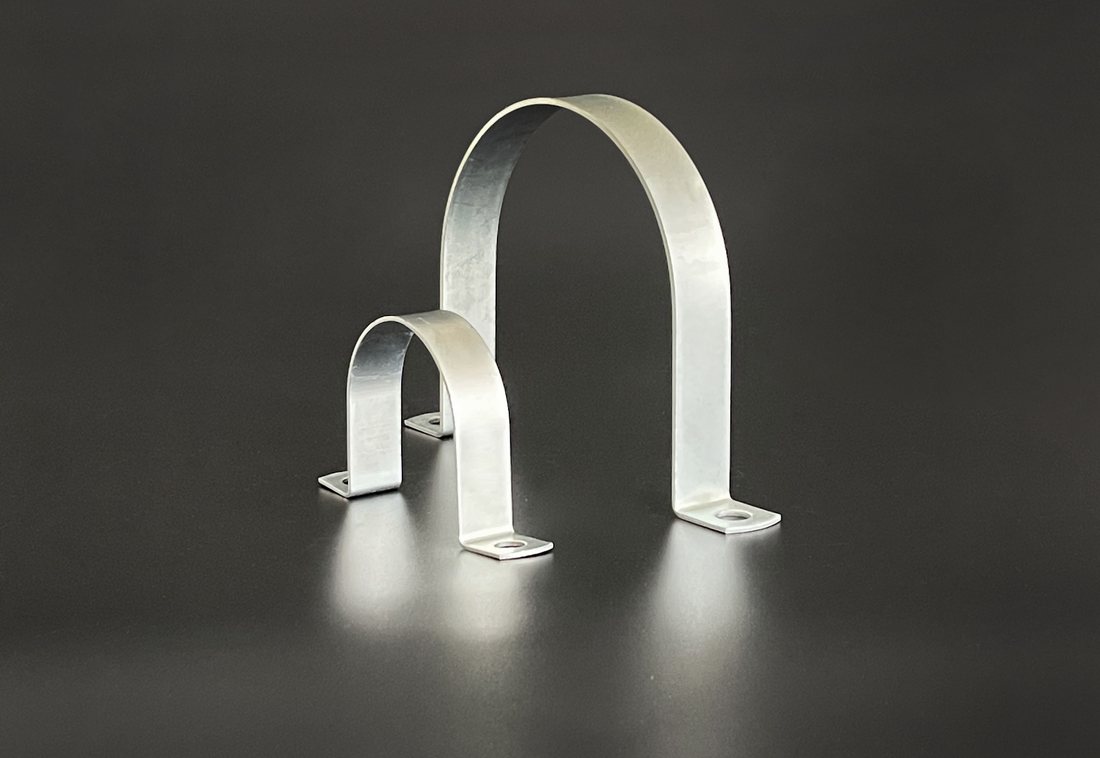
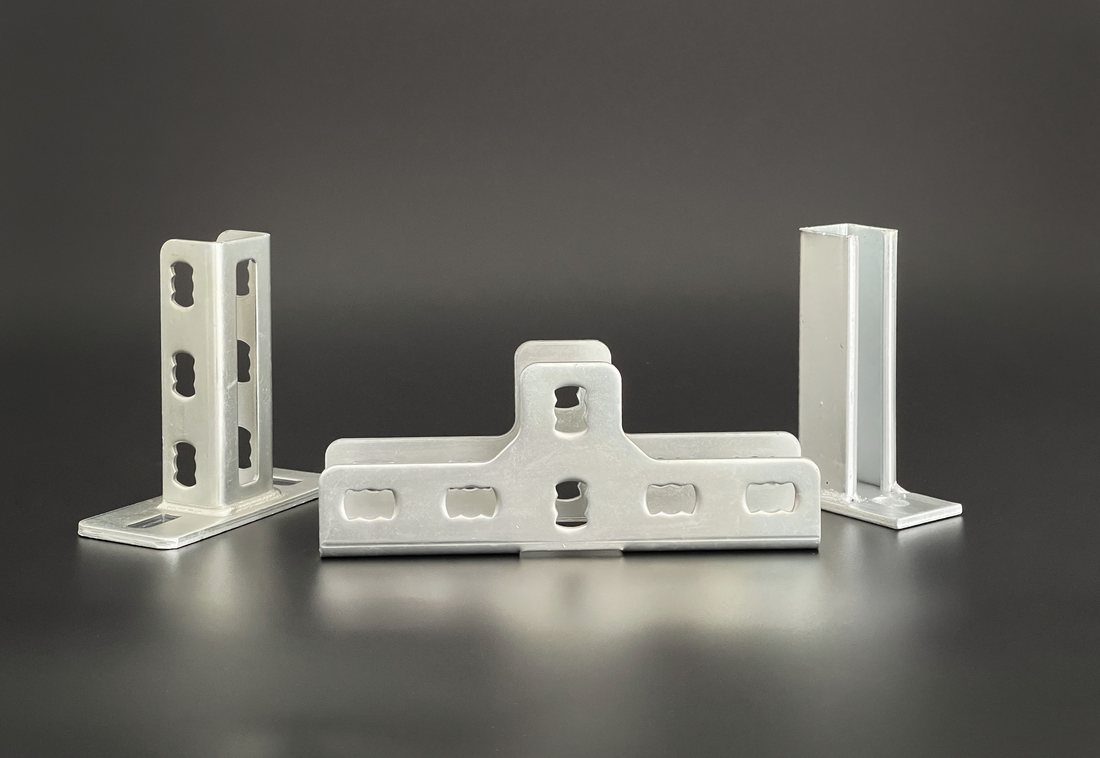
| Conduit saddles · Clamps · Hangers | Indoor / Outdoor | Innozinc | High-mix, small-batch production · Barrel plating available |
| Grounding components · Bonding hardware | Electrical continuity requirements | Innozinc | Assembly-specific contact-resistance testing and specification development |
| Transmission-tower fasteners | Continuous outdoor exposure · High elevations | Innozinc-h | SST 1,500–2,000 hr |
| Coastal and island distribution hardware | Salt exposure and dissimilar-metal contact | Innozinc-h | Galvanic corrosion: rated Very Good · Acid resistance: rated Good |
| Products with specified surface-treatment requirements | — | Specification alignment | Specification revision or equivalent-performance approval incorporated into the adoption process |
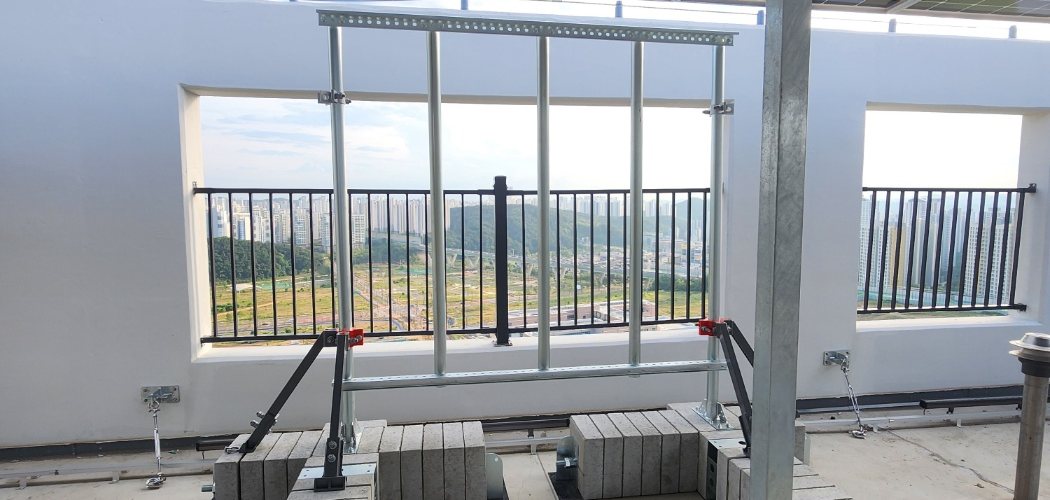
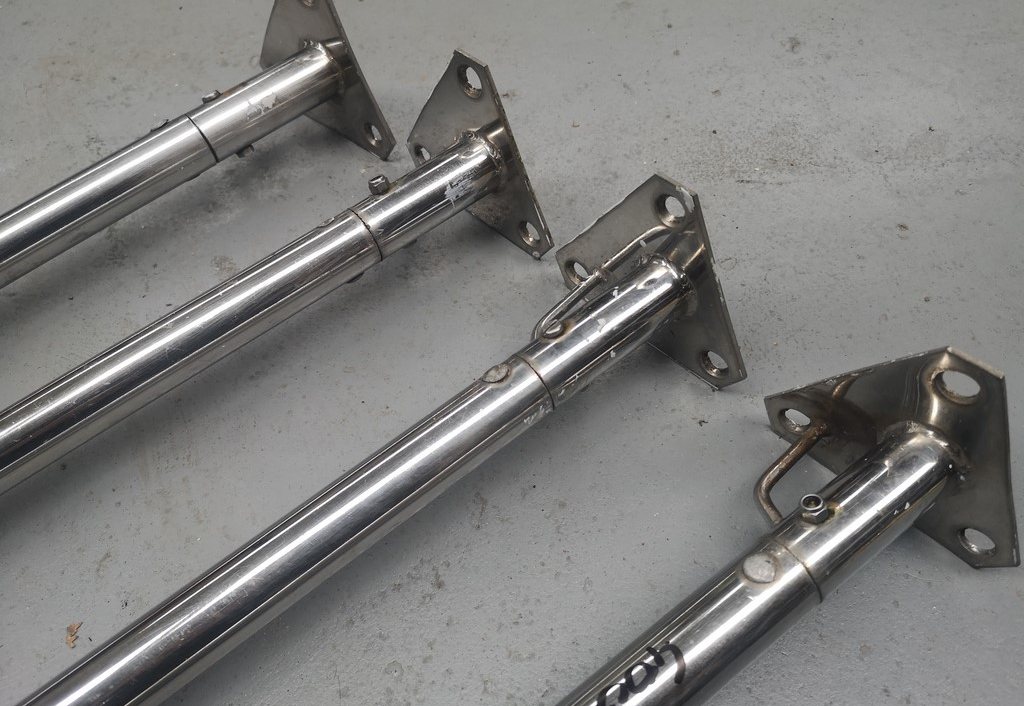
Product drawings and exposure conditions guide the surface-treatment specification, assessment criteria and supply conditions.
Representative SST specifications are 720–1,000 hr for Innozinc and 1,500–2,000 hr for Innozinc-h, supporting product-specific corrosion requirements.
Target thickness and inspection conditions reflect thread tolerances, mating materials and downstream fabrication methods.
KEMP supports surface-treatment specification and equivalent-performance approval requirements with technical data and sample testing.
Power-hardware performance assessment and experience with telecommunications supports and fastening structures inform product-specific plating design.
Plated specimens, U-bolts and shackles met the targets for corrosion resistance, formability, abrasion resistance and tensile-load performance.
U-bolts and shackles: no red rust after 600 hr neutral salt spray and 40 cyclic-corrosion cycles. No surface defects at a tensile load of 39.20 kN.
Telecommunications support and fastening applications inform geometry-specific plating and quality-control plans.
Technical guidance on specification selection, quality control and production implementation for power hardware.
Discover KEMP surface-treatment solutions for industry-specific exposure conditions and product requirements.
