Contact-interface design
Mating materials, contact surfaces and tightening torque define galvanic-corrosion controls and contact-resistance assessment conditions.

Innozinc Ceramic Galvanizing improves corrosion resistance and downstream fabrication quality in grating, trenches, seismic supports, conduit clips and fasteners. Its thin deposit supports dimensional control and integration with bending and welding operations. Supply experience in Korean petrochemical, biopharmaceutical and display projects informs specifications for building and utility steelwork.
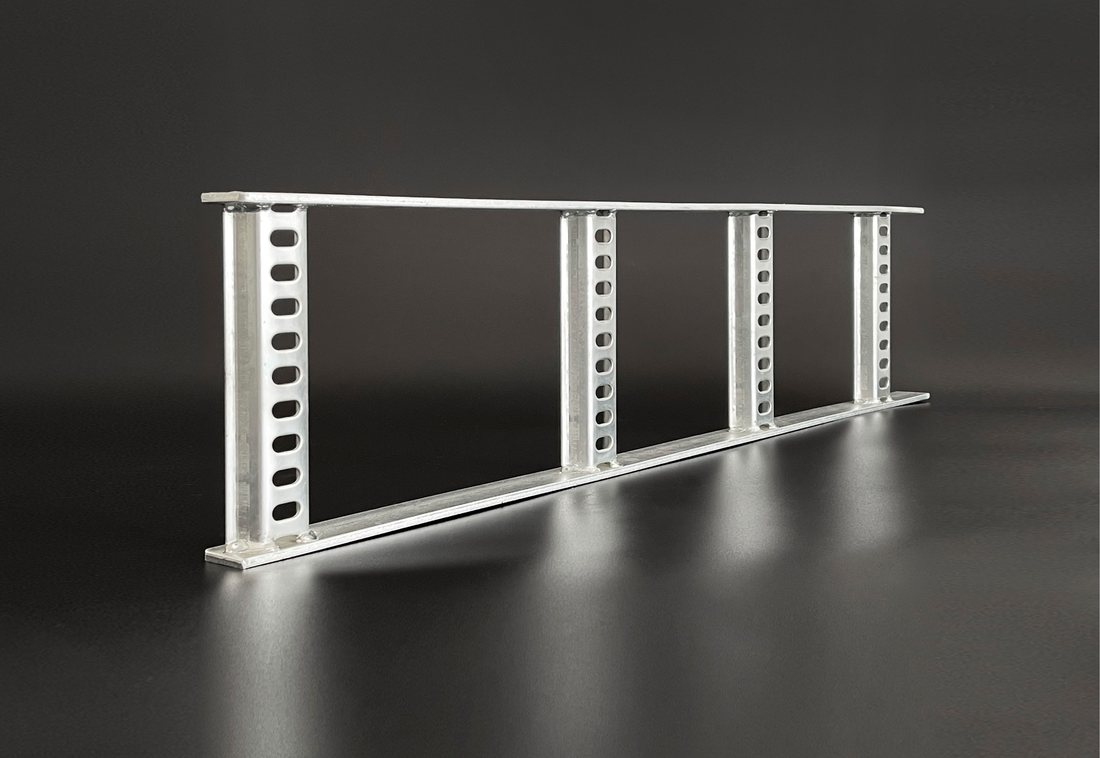
Building and utility steelwork requires corrosion protection together with fastening tolerances and downstream fabrication quality. KEMP designs the plating process around component geometry and installation conditions.
Pipe supports and fasteners require coordinated control of plating thickness, geometric precision and fabrication quality. Innozinc's thin deposit supports assembly tolerances and downstream processing.
Thickness variation affects connection gaps and threaded assembly tolerances. Innozinc uses controlled electrodeposition to manage product-specific dimensions.
Steel fittings and fastenersIn KEMP's in-house assessment, the Innozinc specimen met the 140° bend requirement. A specimen touched up after bending showed no defects after 2,640 hr salt spray exposure. Post-treatment is applied according to coating condition on the tensile side of the bend.
Post-plating fabricationInnozinc supports welding without prior removal of the plated layer; the cited radiographic assessment reported no defects. Local repair in the documented process covered 3–5 cm around the weld. Adjacent zinc provides sacrificial protection at exposed cut edges.
EPC fabrication sequence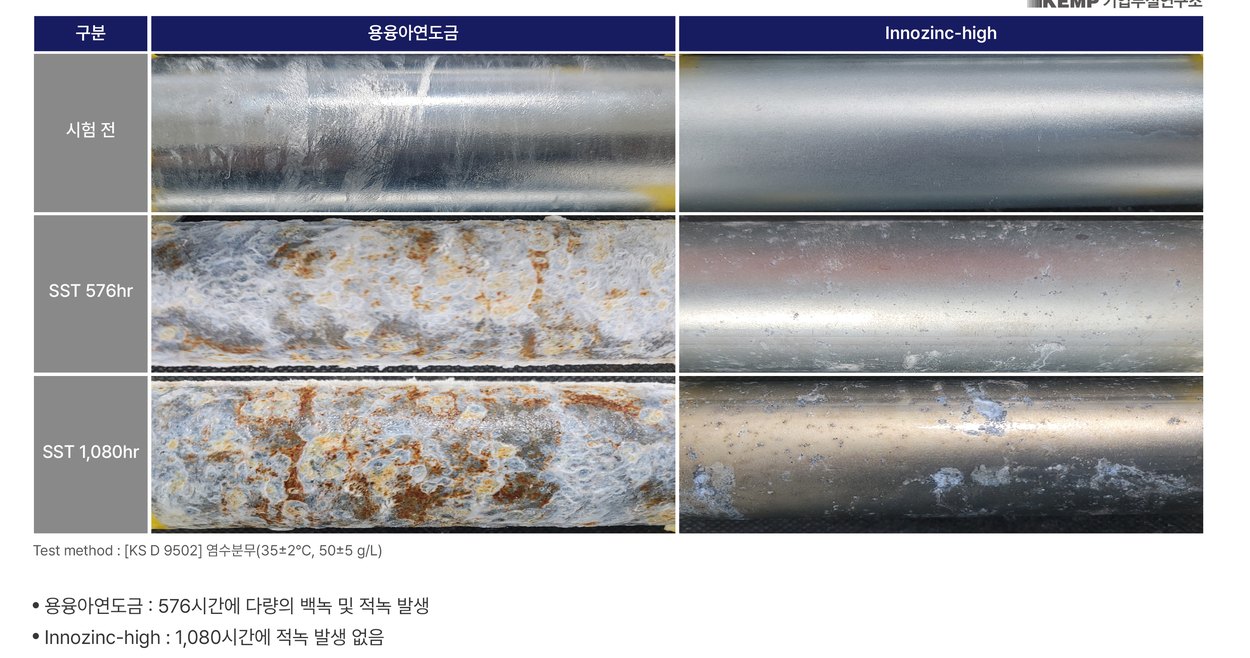
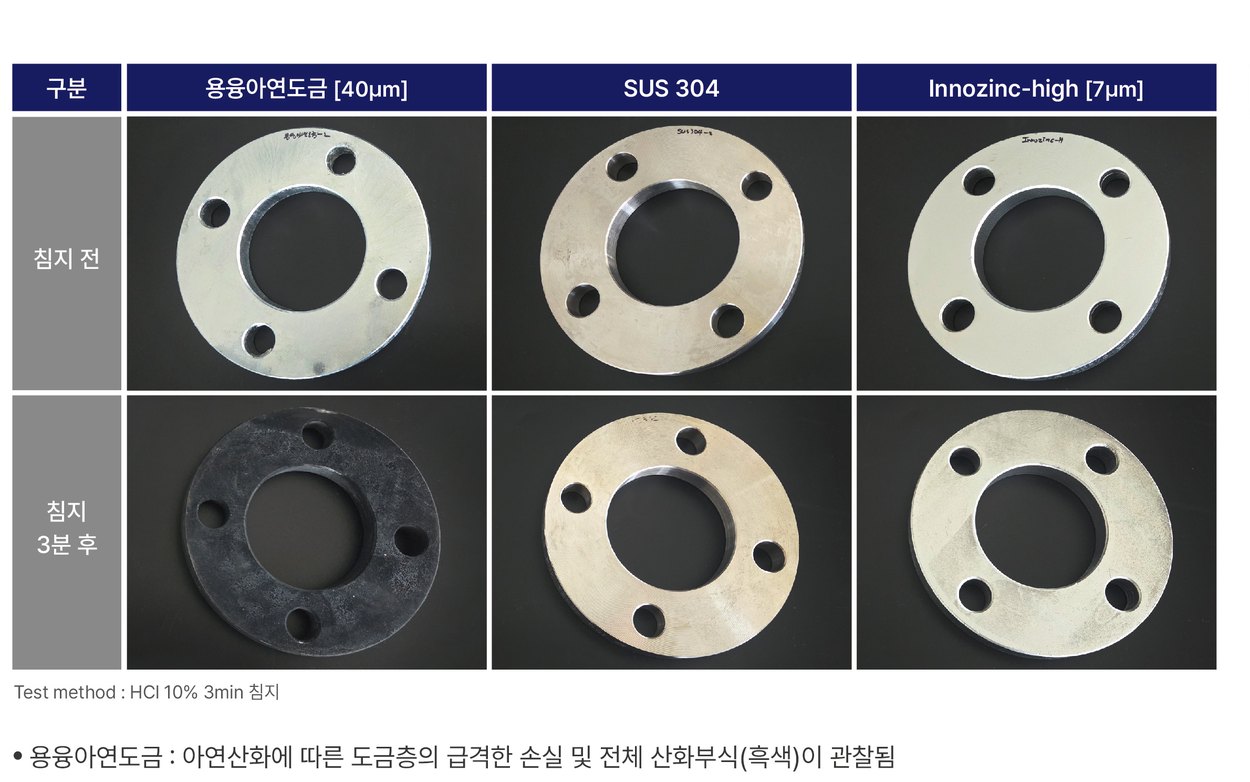
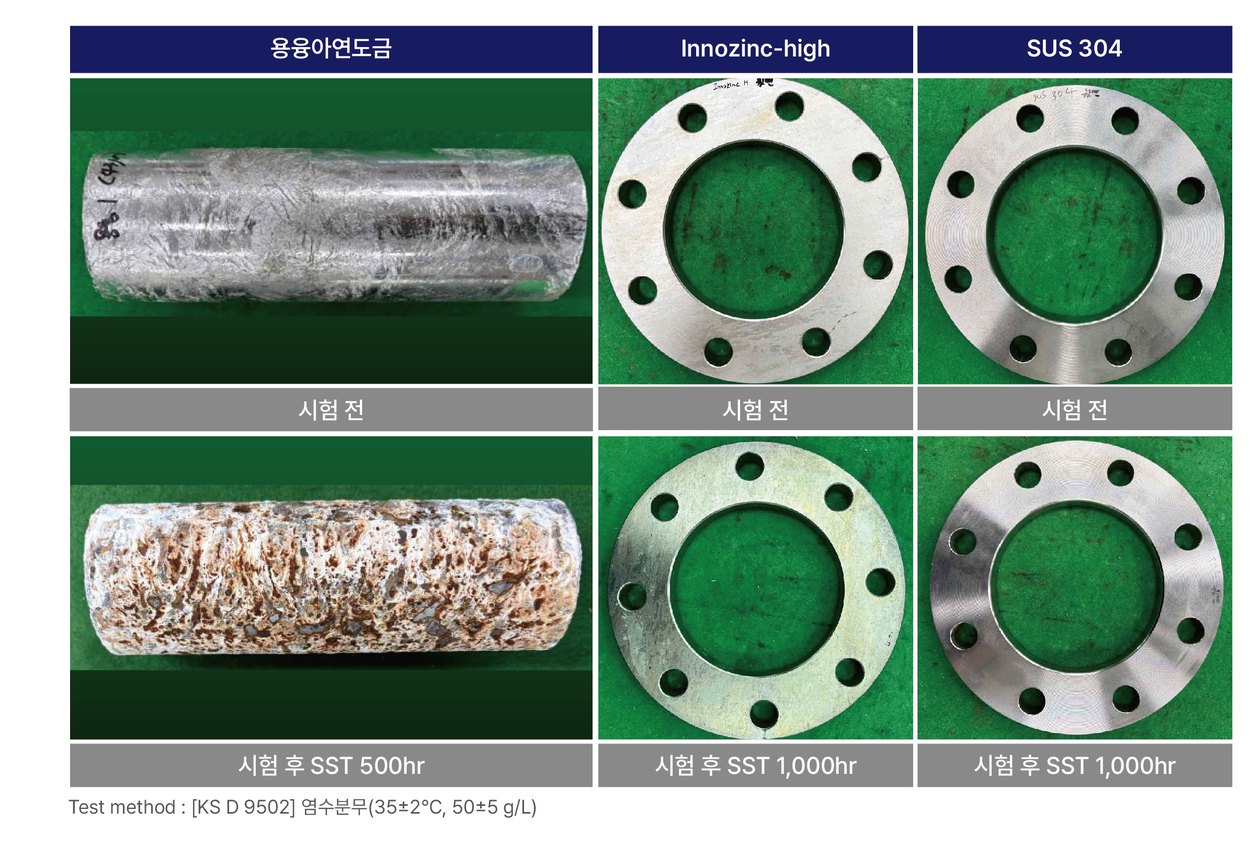
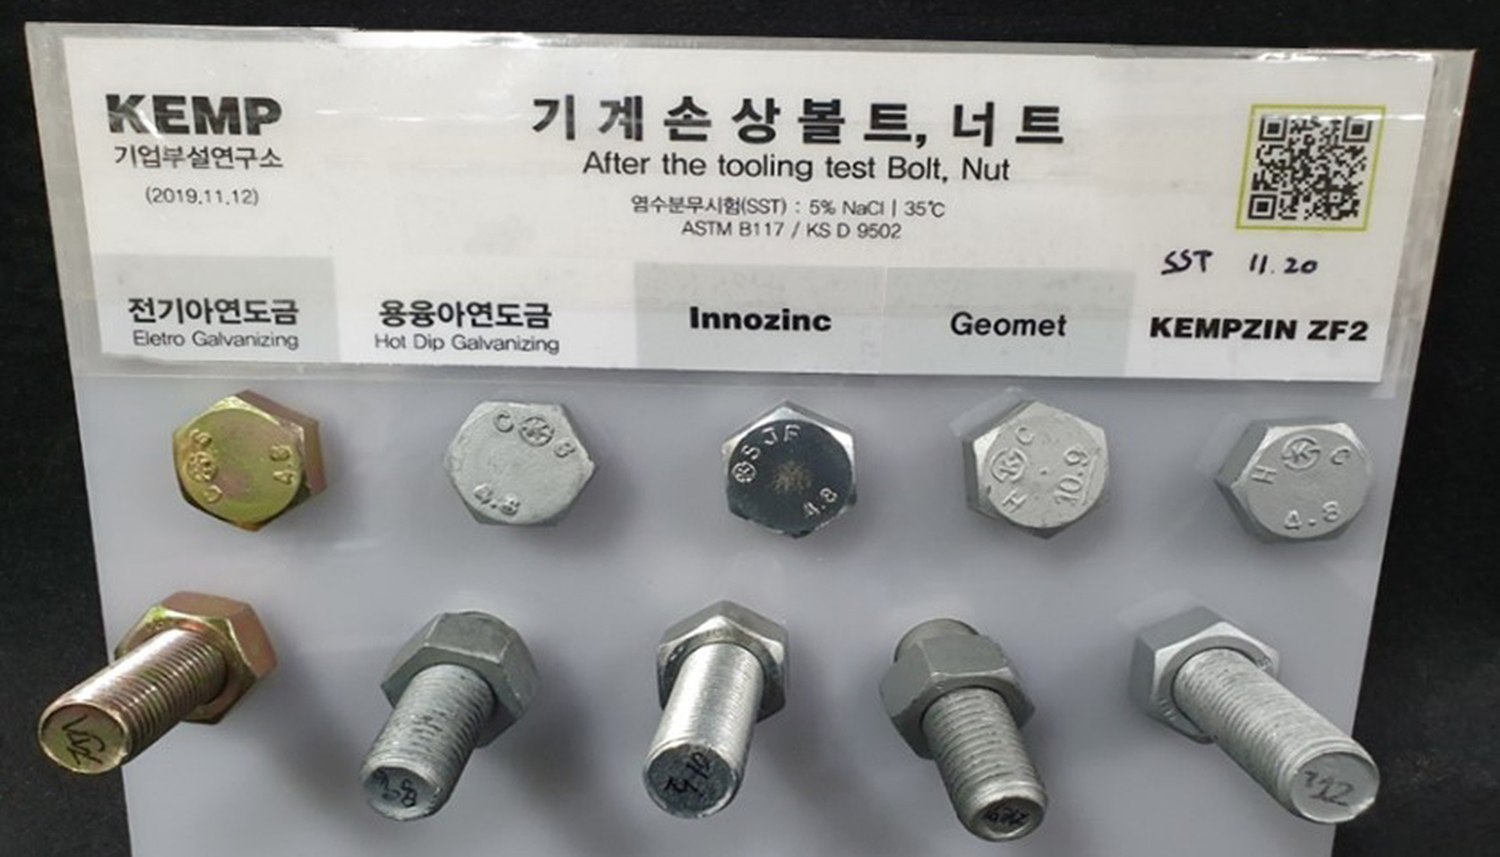
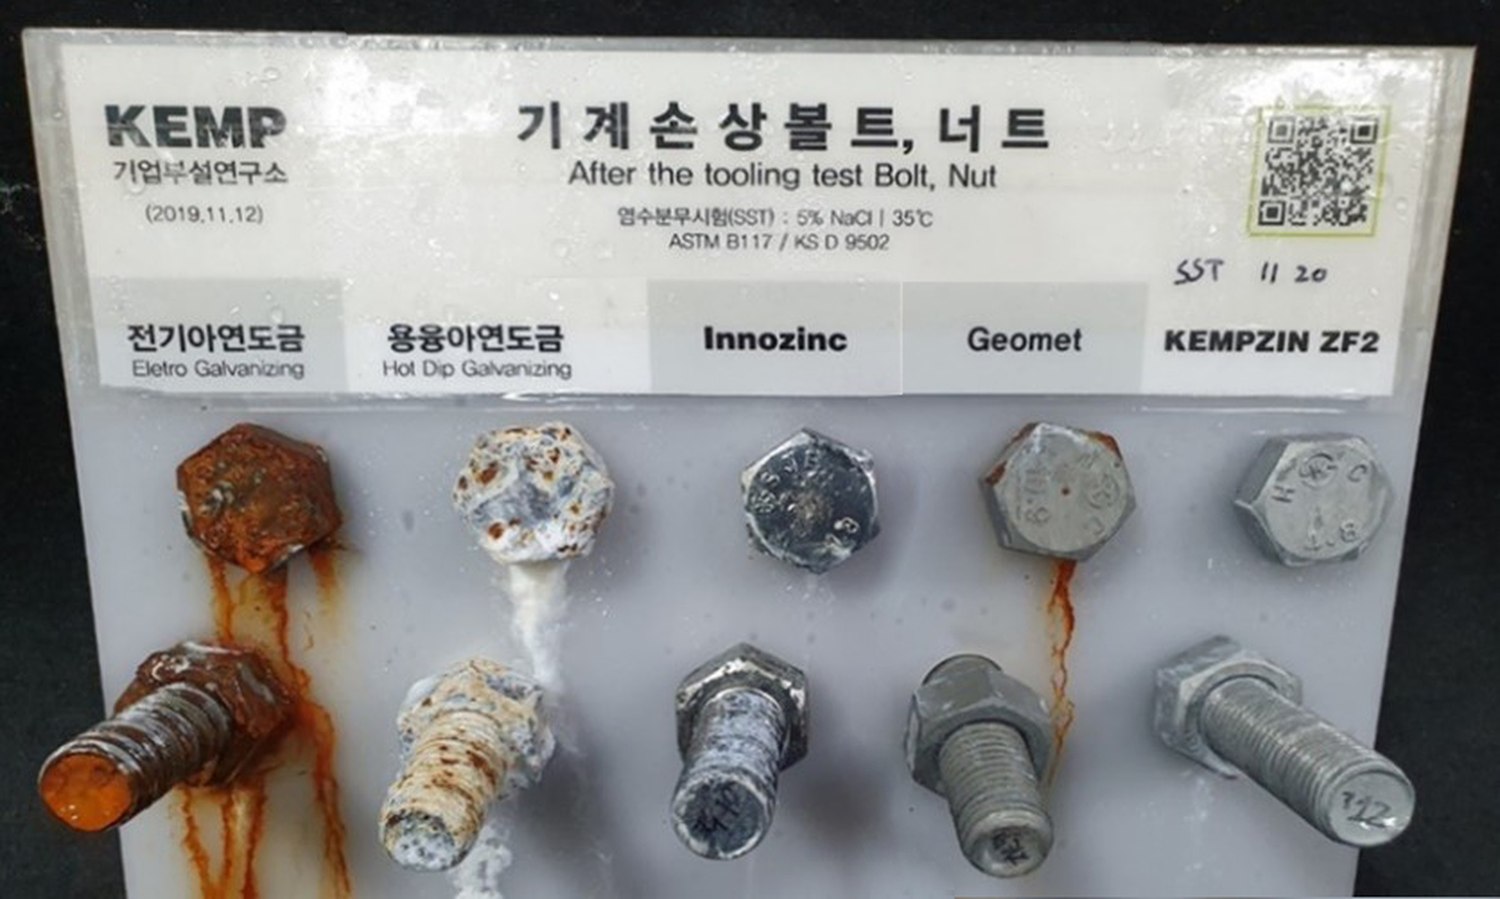
KEMP R&D photographs document in-house comparative assessments. Each specimen's coating, mechanical-damage condition and exposure period define the corrosion and coating-integrity observations.
| Characteristic | Hot-dip galvanizing | Innozinc Ceramic Galvanizing | Test / Data Source |
|---|---|---|---|
| Nominal coating thickness | 50 ~ 100 μm | 8 ~ 20 μm | Specification value |
| Coating thickness distribution | Variation associated with immersion and drainageObserved pipe-connection gap up to 240 μm | Controlled thin deposit | Specification and field observations |
| Pipe salt spray exposure | Extensive white/red rust at 576 hr | No red rust at 1,080 hr | KEMP in-house test |
| Pipe fitting salt spray exposure | White and red rust across the surface at 480 hr | Dark corrosion products across the surface at 800 hrNo white or red rust | KEMP in-house test |
| Bolt-and-clip salt spray test in the assembled state | Single-system assessment | Slight white rust at 384 hr · No red rust at 2,664 hr | KEMP in-house test |
| Seismic supports / hangersReference: zinc electroplating | Zinc electroplating: red rust at 192 hrExtensive red rust at 456 hr | Assembly: no red rust at 456 hrSeparate component: slight red rust at a rivet nut at 936 hr | KEMP in-house test |
| Bending after plating | Cracking in the cited test | 140° bend requirement metAfter bend-area touch-up: no defects at 2,640 hr SST | KEMP in-house test |
| Welding without stripping the plated layer | Masking, hole preparation, deburring and touch-up operations | Welding without prior strippingLocal repair within 3–5 cm of the weld | KEMP in-house test |
| Adhesion (cross-cut) | Equivalent — ASTM D3359 | Third-party test laboratory | |
| Pencil hardness | Equivalent — ASTM D3363 | Third-party test laboratory | |
| Abrasion resistance and formability | Innozinc advantage — ASTM D4060 · KS B 0812 | Third-party test laboratory | |
Building and utility steelwork is assessed for corrosion resistance, dimensions and fabrication quality. Electrical interfaces are assessed under representative assembly conditions.
Mating materials, contact surfaces and tightening torque define galvanic-corrosion controls and contact-resistance assessment conditions.
Inspect coating thickness, adhesion and surface condition, then manage coating integrity after bending, welding and cutting.
Customer drawings and inspection specifications guide sample production and assessment of assembly fit, appearance and corrosion resistance.
Explore fastener supply records for petrochemical, biopharma and display facilities, together with building and utility plating applications.
| Product | Application | Supply / Assessment Record |
|---|---|---|
| Bolts · Nuts · Washers | Structural and equipment anchorage | Production supply: petrochemical seismic U-bend components, 44,000 kg (since Nov 2024); biopharma cooling-tower bolts, 12,000 kg; display-facility structural bolts, 5,000 kg |
| Grating and conduit fixing clips | Walkway and conduit supports | In-house assembled-specimen test: no red rust after 2,664 hr SST |
| Seismic supports and hangers | Pipe and equipment supports | In-house comparative testing completed |
| Steel grating and low-noise trench systems | Walkways · Platforms · Drainage | Performance test data submitted · Application specifications under discussion |
| Nominal 50A pipe and fittings | Utility piping | Plating trials completed · Specification support for pipe lengths up to 3 m |
| Cable trays and brackets | Power, telecommunications and piping supports | Plating specifications based on geometry, dimensions and exposure |
Define plating requirements and assessment items for the material, geometry and service environment.
Assess corrosion resistance, fabrication capability and assembly quality on actual components.
Incorporate customer inspection criteria and initial assessment results into each product specification.
Operate plating and inspection processes to the agreed production volume and delivery schedule.
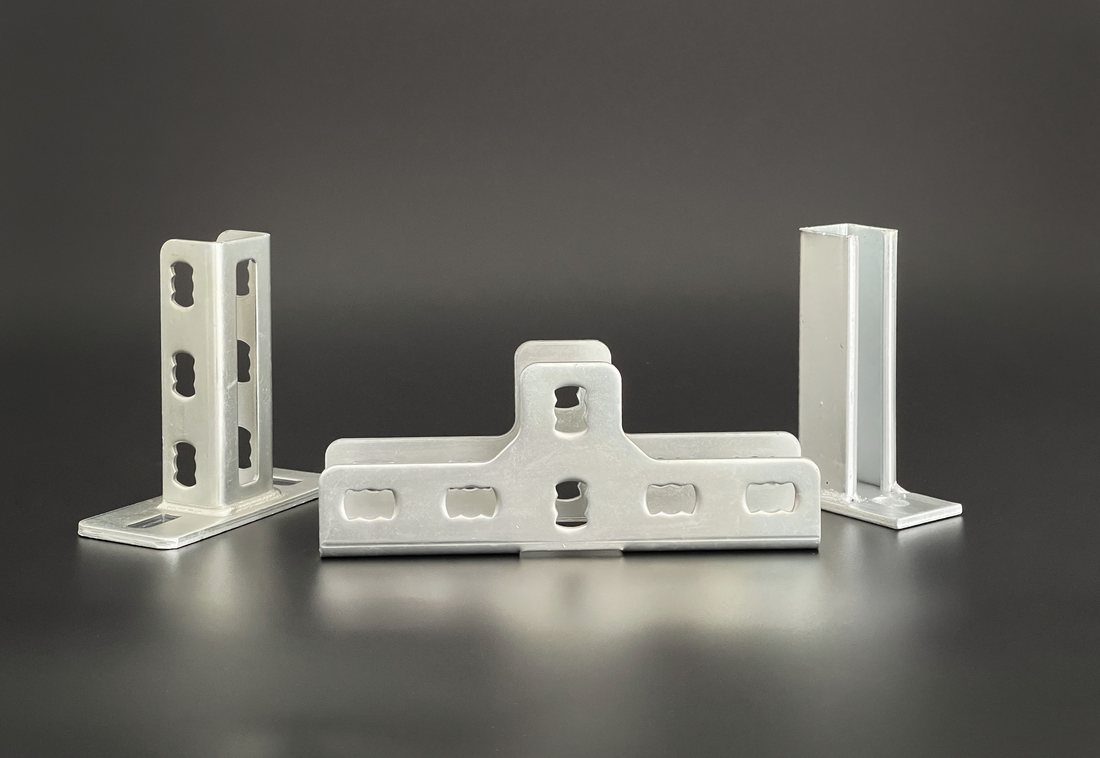
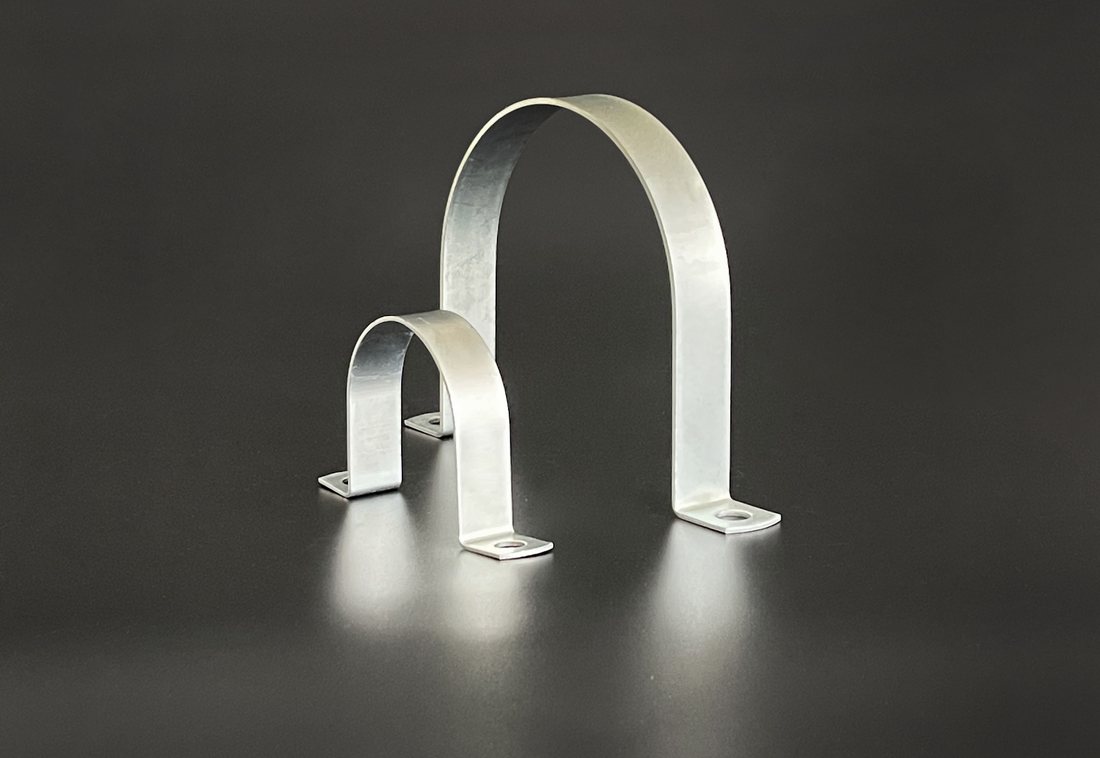
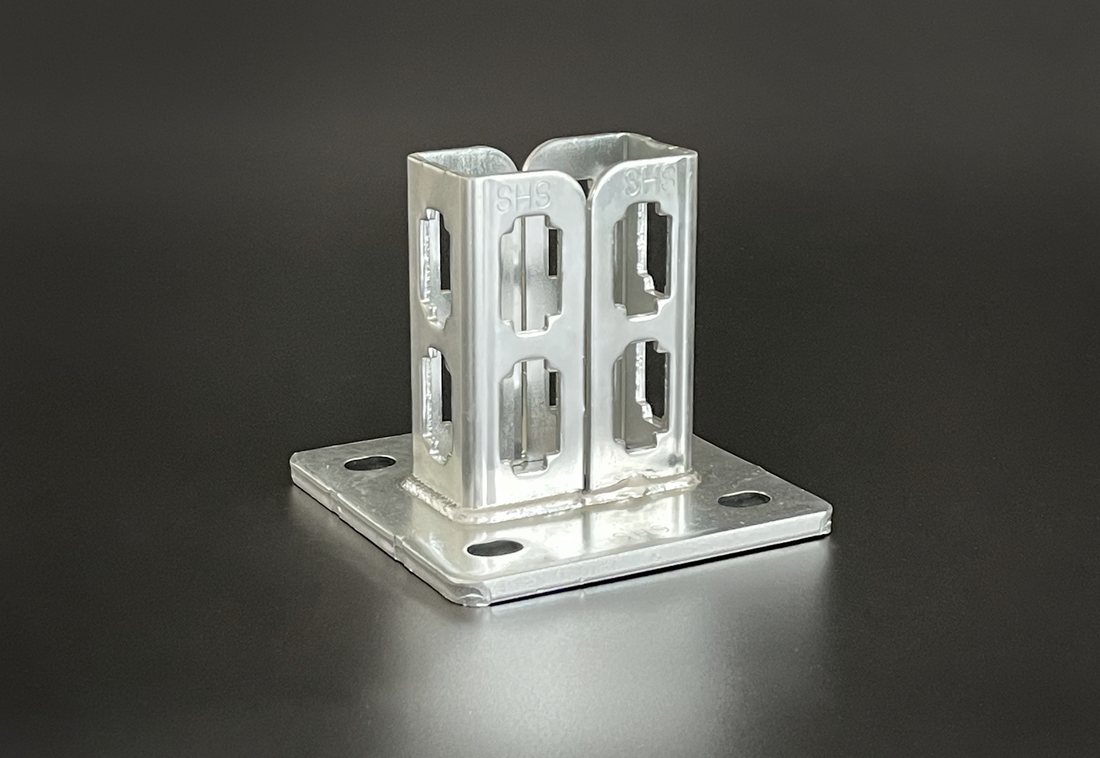

Design requirements and process conditions are coordinated for general structural, support and fastening components.
General fastener specifications focus on property class 8.8 and below. High-strength components undergo hydrogen-embrittlement control planning and process qualification before production.
Mating materials, contact-area ratios and moisture ingress determine insulation, sealing and plating specifications.
Service temperature and exposure to chemical environments define product specifications and assessment criteria. The substance, concentration and contact duration are considered together.
Applications include building and utility grating, trench systems, supports, hangers, conduit clips and general fasteners. Plating specifications are based on drawings, material, strength grade and service environment.
Innozinc's thin deposit supports downstream fabrication. The cited in-house test met the 140° bend requirement. Post-treatment, including touch-up on the tensile side, reflects the coating condition after forming. Welding procedures follow the working conditions and safety instructions.
KEMP provides supply examples for petrochemical seismic U-bend components, bolts for cooling towers at new biopharma facilities, and display-facility structural fasteners. Grating, trench and piping applications are supported with product-specific performance data and specifications.
Electrical performance is assessed on the actual assembly, including contact surfaces, tightening torque and mating materials. The program covers contact resistance after corrosion and environmental exposure against customer inspection requirements.
Send drawings or photographs, material, dimensions, quantity and installation environment. Our team will confirm the plating specification and sample quantity, cost and schedule.
Discover KEMP surface-treatment solutions for industry-specific exposure conditions and product requirements.