UP100-A · UP100-AW
Premix UP100-A and UP100-AW at 1:1, then dilute 1 part mixture with 100 parts water.
KEMP · ELECTROGALVANIZING UPGRADE
 Upgrade 100
THIN COATING · BASIC UPGRADE
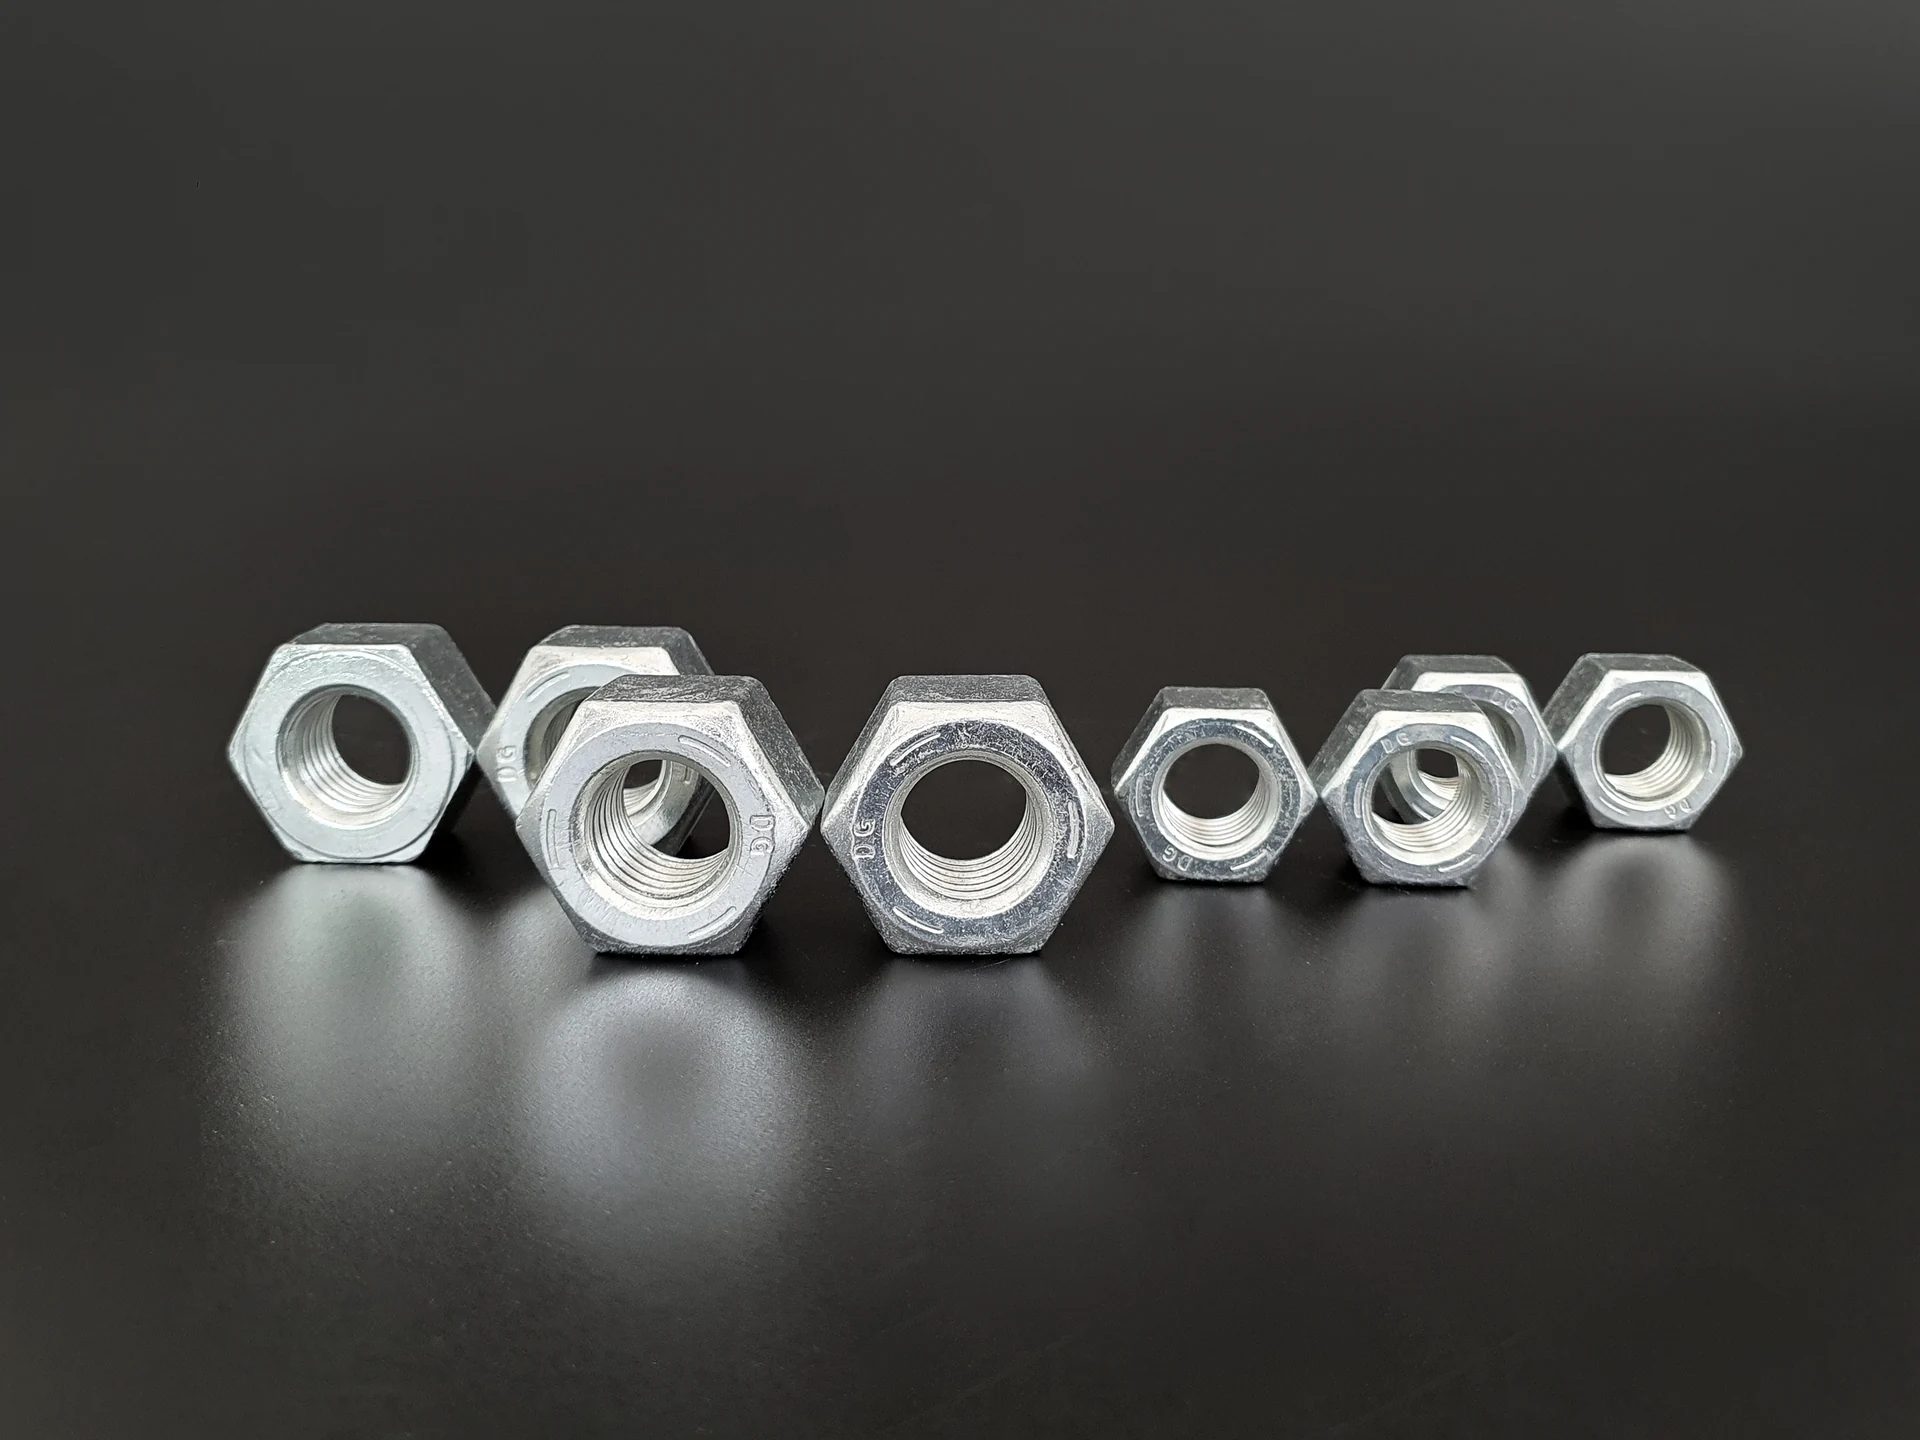
ELPANG Upgrade 100 · Coating thickness Approx. 1 μm · White-rust SST 15 hr · Red-rust SST 96 hr. Review the thickness-specific performance table and evaluate actual components under the intended process conditions before use.
Review the thickness-specific performance table and evaluate actual components under the intended process conditions before use.
PERFORMANCE BY THICKNESS
Compare white- and red-rust SST results
at each plating thickness to select
the specification for your components.
On smaller screens, scroll horizontally within the table to view all columns.
| Grade | Existing zinc electroplating | After ELPANG application | ||||
|---|---|---|---|---|---|---|
| Thickness (µm) | White-rust SST (hr) | Red-rust SST (hr) | Thickness (µm) | White-rust SST (hr) | Red-rust SST (hr) | |
| Upgrade 100 | ≈1 | 5 | 24 | ≈1 | 15 | 96 |
Source documents supplied on 2026-10-01. Each row is an application reference for a different thickness condition, not a maximum-hour guarantee at every thickness. The baseline is unsealed for 100 and sealer-treated for 300/500. Control zinc plating, trivalent passivation and post-treatment, and test actual parts before application. SST hours do not represent service life.
PRODUCT & PROCESS
Review pretreatment, plating and post-treatment conditions on the existing line against the customer's specification.
Premix UP100-A and UP100-AW at 1:1, then dilute 1 part mixture with 100 parts water.
Premix UP100-B and UP100-BW at 1:1, then dilute mixture:water at 1:15 for rack or 1:10–15 for barrel.
Technical documentation is available for detailed specifications and application processes.
Review the thickness-specific performance table and evaluate actual components under the intended process conditions before use.
APPLICATION REVIEW
Share the substrate, plating thickness and target corrosion resistance. KEMP will recommend an Upgrade 100 application process and chemical specification. Refer to the latest technical data sheet (TDS) for detailed operating conditions.